Start Your Electric Toothbrush Project
Tell us your product requirements and target market. We will review the details and reply with the relevant next steps.
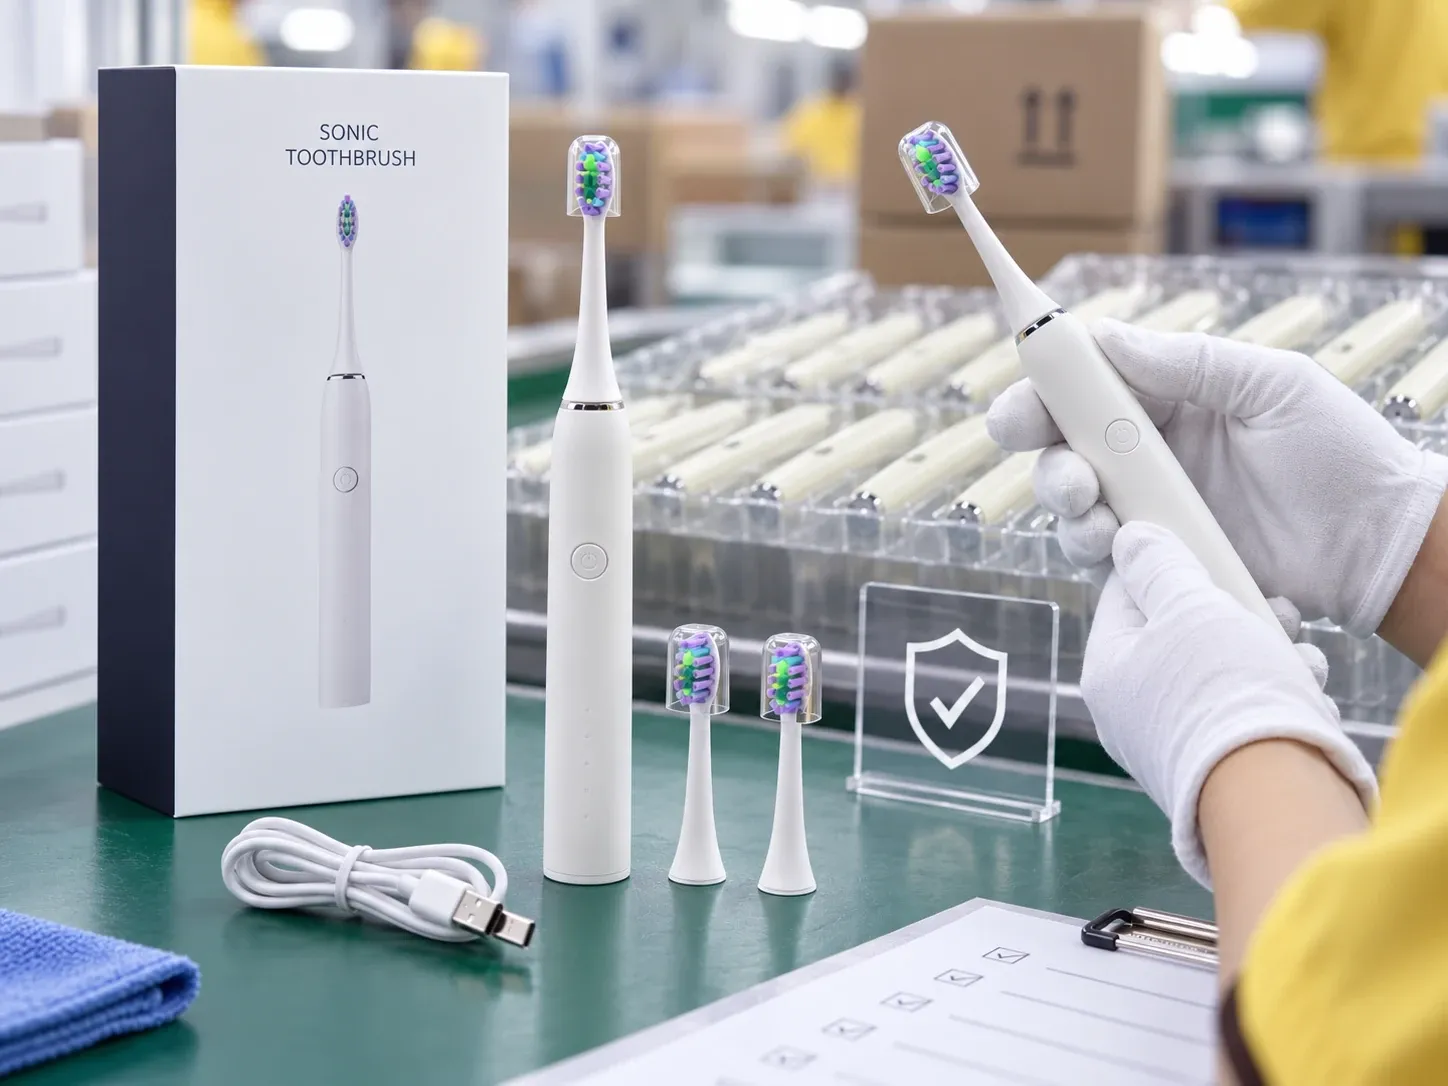
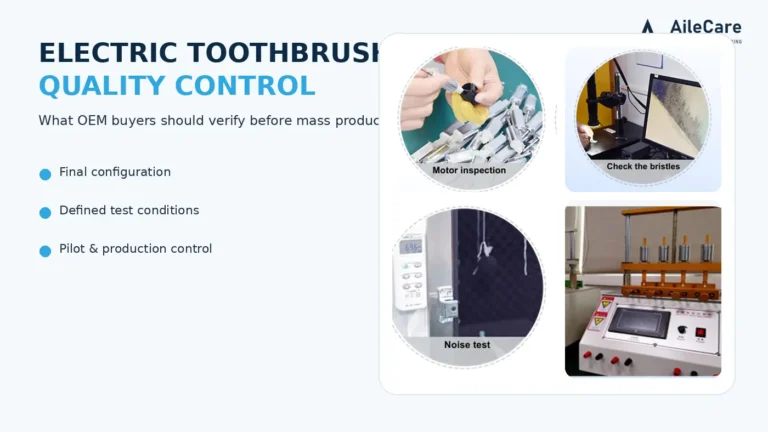
Incoming inspection controls what enters production. In-process inspection controls how the product is being built. Final or pre-shipment inspection checks whether finished goods match the agreed release criteria.
None of these stages works well on its own. Inspection can only compare a product against requirements that have already been defined.
This guide explains what B2B buyers should define before mass production of electric toothbrushes, replacement brush heads, or water flossers, which checks typically belong at each stage, and what final inspection cannot prove.
“Good quality,” “good fit,” “strong vibration,” “no leakage,” and “premium appearance” are expectations, not inspection standards.
Two inspectors can look at the same unit and reach different conclusions if there is no defined point between acceptable and defective.
Before mass production, the following should normally be locked and version-controlled where applicable:
A brush head that should “fit well,” for example, is difficult to inspect consistently.
A project-defined requirement can instead identify the compatible handle, the insertion and removal method, unacceptable looseness or interference, and the reference sample used for comparison.
The first approach invites disagreement. The second gives the buyer, factory, and inspector a common basis for the same pass/fail decision.
If the project is still at the specification stage, it helps to prepare an oral-care product brief before contacting an OEM supplier so these requirements exist before sampling and production planning begin.
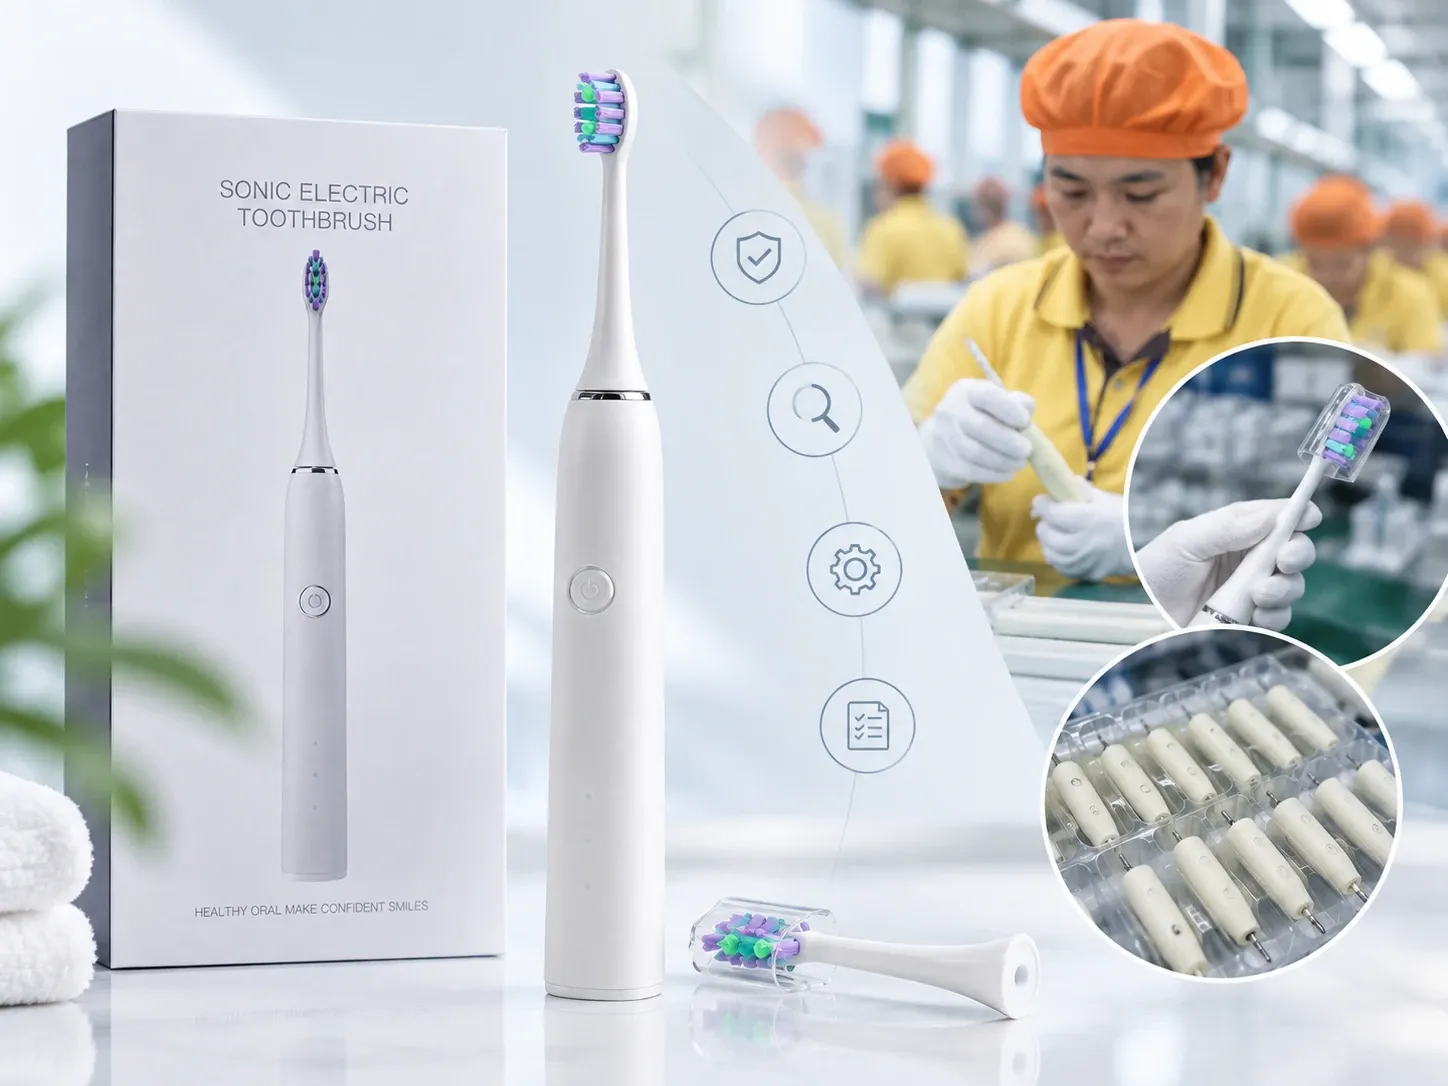
Incoming Quality Control, or IQC, checks whether received materials, components, and packaging match approved requirements before they are released to production.
Its role is to stop incorrect or defective inputs early, before they become assembled finished goods.
Incoming checks commonly fall into five groups:
The examples below are planning references rather than a universal checklist.
| Component / Material | Typical Incoming Check | Why It Matters |
|---|---|---|
| Housings | Part number, color, surface finish, key dimensions | Cosmetic and fit problems multiply once assembly starts |
| Motor / drive components | Model, supplier lot, sample functional check where defined | A wrong motor batch may still power on but perform differently |
| Rechargeable battery | Approved model and supplier, lot, labeling, documentation | A finished unit may charge even if the battery is not the approved version |
| PCB / electronics | Board revision, supplier, lot, appearance | Revision errors may be invisible after assembly |
| Seals / O-rings | Dimensions, appearance, lot | Incorrect or damaged seals may create later leakage risks |
| Brush heads / bristle materials | Model, interface, bristle color, appearance, lot | Interface and tufting inputs affect fit and bristle-retention risk |
| Pump, tubing, valves, tank | Part identity, dimensions, cleanliness, orientation-critical parts | Water-path components may create hidden leakage points |
| Charging components | Model, plug or interface version, labeling | Market-specific configurations are easy to mix |
| Packaging materials | Artwork revision, barcode, printing quality, quantity | A correct product in the wrong packaging version still fails the order |
Incoming inspection does not mean every component receives laboratory testing.
It controls production inputs. It does not prove that later assembly, final packaging, reliability, or market compliance will be correct.
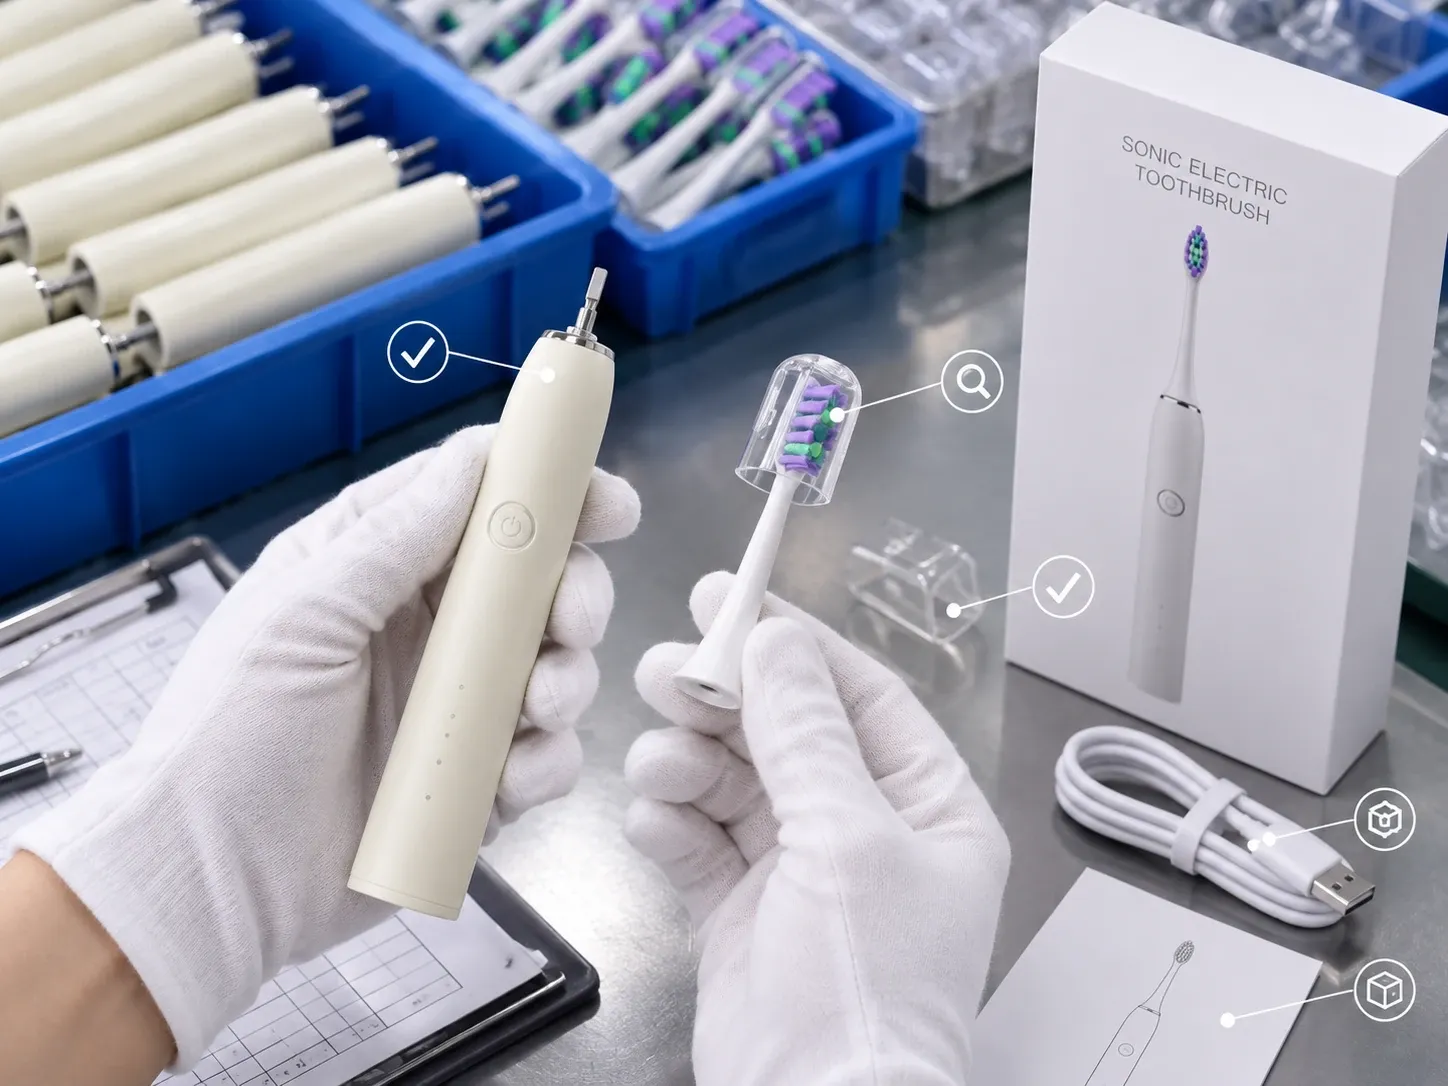
In-Process Quality Control, or IPQC, monitors the product while it is being manufactured and assembled.
Common approaches include:
The exact method and frequency are supplier- and project-dependent.
Typical process-stage controls may include:
These controls are useful because some problems become difficult to identify after final assembly.
Typical process controls may include:
Where several similar brush-head models are produced on the same line, model and interface control becomes particularly important.
Typical process-stage controls may include:
The buyer-side lesson is simple: some risks should be controlled while the product is being built.
A misplaced O-ring, incorrect PCB revision, wrong valve direction, or drifting assembly process may be difficult to detect reliably after the finished product has already been packed.
Final inspection may still identify some of these problems, but by then it may be much harder to determine how many units are affected.
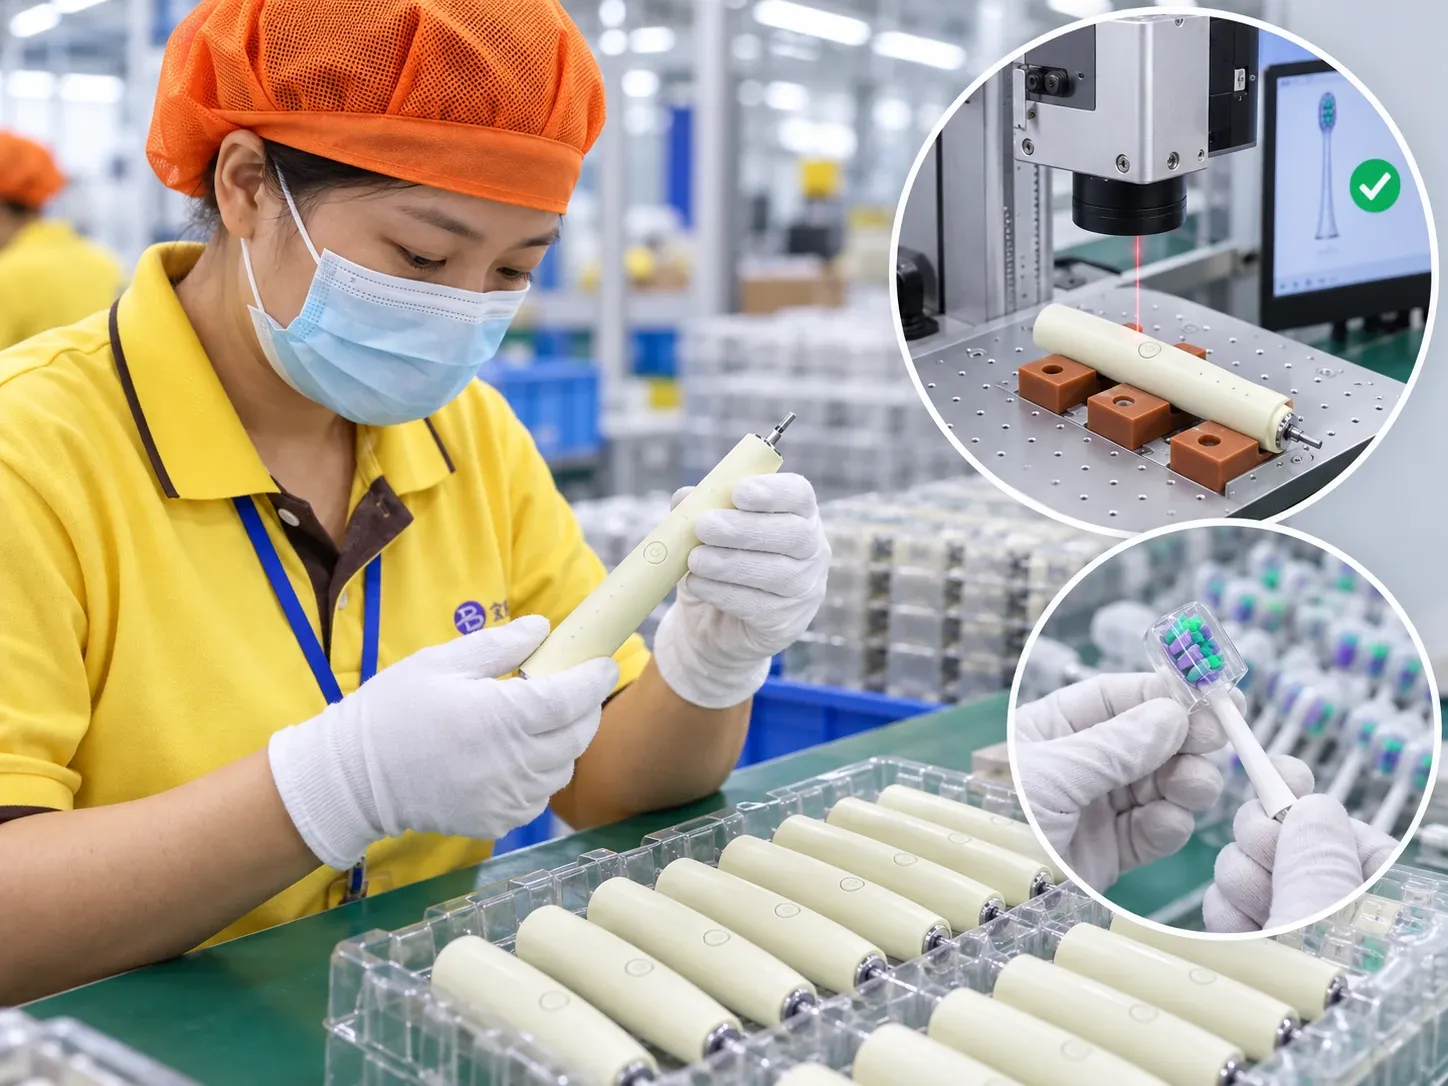
FQC, OQC, final inspection, Final Random Inspection, and Pre-Shipment Inspection often overlap, but different factories and inspection providers may use the terms differently.
FQC commonly refers to finished-product inspection. OQC often refers to outgoing release control. PSI or FRI commonly refers to a sampling inspection when an order is substantially complete and packed.
Instead of relying on the terminology alone, buyers should define the actual scope.
Confirm:
Finished-goods inspection may review:
These should be judged against approved criteria or reference samples rather than personal opinion.
For electric toothbrushes, typical short-duration checks may include:
For water flossers, checks may include:
These are short functional checks.
They should not be presented as endurance, lifetime, waterproof certification, or long-duration performance testing.
Final checks may also confirm:
A functional product can still fail an order if the wrong accessory, color, model, or regional configuration is packed.
Final or pre-shipment inspection may also cover:
This is why packaging artwork and label planning should be finalized and revision-controlled before production reaches the shipment stage.
A passed pre-shipment inspection provides sampled evidence that the inspected units met the agreed criteria at a particular point in time.
It does not prove that:
PSI is an important release check, but it cannot prove everything about the design, production history, or long-term performance of the product.
AQL, or Acceptance Quality Limit, is used as part of an acceptance-sampling system, commonly based on ISO 2859-1 or ANSI/ASQ Z1.4.
Lot size, inspection level, the selected sampling plan, and the selected AQL help determine the sample size and the acceptance or rejection numbers.
Two common terms are:
AQL does not mean that a shipment is guaranteed to contain no more than that percentage of defective products.
It is part of an acceptance-sampling decision system. Products that were not selected for inspection were not individually verified.
Defects are commonly divided into categories such as:
Critical
A safety, regulatory, or otherwise unacceptable risk as defined for the project.
Major
A defect that materially affects function, usability, assembly, salability, or another important agreed requirement.
Minor
A deviation from the agreed standard that does not significantly affect normal use.
The classification should be project-defined.
A leak, scratch, missing label, or fit problem may carry different severity depending on the product, market, intended use, and brand requirements.
The frequently seen combination:
Critical 0 / Major 2.5 / Minor 4.0
is a common commercial example in consumer-goods inspection.
It is not a universal mandatory rule for oral-care products.
The buyer and supplier should agree defect classifications and sampling criteria based on the specific project before production begins.
The approved sample should be a physical reference, not the only quality standard.
A Golden Sample or approved sample is useful because it gives the buyer, factory, and inspector a physical reference for characteristics that are difficult to communicate only through text.
However, it cannot replace controlled written specifications.
| Reference | Best Used For | Cannot Define Alone |
|---|---|---|
| Approved sample | Appearance, color, finish, configuration, visible assembly, accessories, packaging presentation, basic user-perceived function | Dimensions, tolerances, BOM versions, material grades, battery specification, PCB/firmware revision, test methods, AQL, reliability and compliance requirements |
| Product specification | Structure, materials, functions, performance targets, test conditions | Physical look-and-feel judgments |
| Approved BOM | Part numbers, component versions, approved suppliers | Finished-product appearance or workmanship |
| Artwork / packaging master | Printing content, revision, barcode, labels, languages | Product function or component control |
| QC checklist | Inspection items, methods, sampling, defect classes, pass/fail criteria | The underlying product design requirements |
These references should use controlled revisions that point to the same approved product configuration.
For the sample-signoff process itself, see our guide to golden sample approval.
Routine production inspection, reliability testing, and compliance testing answer different questions.
None replaces the others.
| Activity | Main Question | Examples | What It Does Not Replace |
|---|---|---|---|
| Routine Production QC | Do incoming parts, work-in-process, and finished goods match defined routine requirements? | Component version, assembly checks, power-on, basic charging, packaging and quantity | Design validation, reliability proof, compliance evaluation |
| Final Functional Inspection | Do sampled finished units work under defined short-duration conditions? | Modes, buttons, indicators, water flow, short functional checks | Lifetime performance, endurance, full waterproof validation |
| Reliability / Validation Testing | Can the design withstand expected use, environment, and lifecycle stress? | Cycle testing, drop testing, battery endurance, long-term sealing or water exposure where applicable | Batch-by-batch release inspection |
| Compliance / Type Testing | Does the product meet requirements applicable to its target market? | Market-specific safety, IP, battery, and regulatory evaluations where applicable | Production consistency control for every batch |
Standards and frameworks such as IEC 60335-2-52, IEC 60529, and UN 38.3 belong to validation, safety, IP-rating, battery transport, or compliance contexts where applicable.
They should not be confused with routine shipment inspection.
A short leakage observation during PSI is not the same as IP-rating verification. A charging check is not battery certification.
For deeper coverage of long-term product performance, see our guide to electric toothbrush reliability testing.
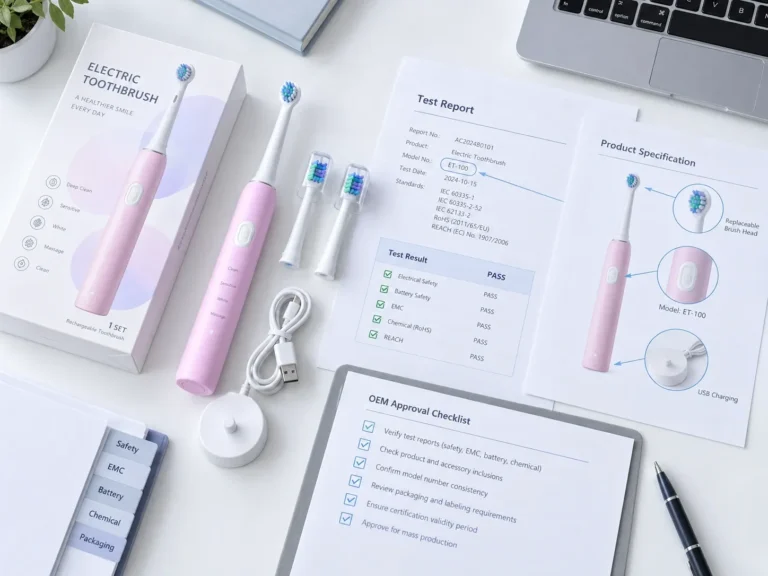
Buyers should also review product test reports separately rather than assuming that a file name alone proves the report applies to the exact product version being ordered.
Before production begins, confirm:
The purpose of this checklist is not to create more paperwork.
It is to make sure everyone is judging the same product against the same requirements.
A visually acceptable sample does not define component versions, tolerances, inspection methods, packaging revisions, or test requirements.
Approve the physical reference together with controlled written requirements.
Sampling rules influence how the shipment will be inspected and released.
Agree them before production, not after finished goods are already waiting for shipment.
Final inspection is a release gate.
It cannot replace controls for incoming parts, assembly processes, material changes, sealing, electronics, or other production-stage risks.
A short sampled inspection confirms only the agreed checks performed on the selected units.
It does not prove cycle life, battery endurance, drop resistance, or long-term waterproof performance.
A new artwork file, cable, brush head, nozzle, instruction manual, or retail box may create a new product configuration.
The controlled inspection documents should be updated accordingly.
If each party works from a different sample, artwork file, specification, or checklist, conflicting inspection results are almost inevitable.
One controlled revision should be used across the project.
Routine QC supports production and batch release.
Compliance and type testing address different questions and may depend on the target market, product configuration, and applicable requirements.
Good OEM quality control is not created by adding more inspections at the end.
It starts with defining measurable acceptance requirements and assigning the right checks to incoming materials, production processes, and finished goods.
Before mass production, align the product specification, approved sample, BOM, packaging version, and inspection checklist.
These references should all point to the same approved product version so that the buyer, factory, and any third-party inspector are working from the same requirements.
For a new oral-care OEM project, define these quality inputs together with the product brief before sampling and production planning begin.
IQC checks incoming materials and components before they enter production. IPQC monitors quality during manufacturing and assembly. OQC commonly refers to outgoing release control before shipment.
The exact boundaries may vary by factory, so buyers should confirm what each stage actually includes.
They often overlap but are not automatically identical.
Final inspection may refer to a factory’s finished-goods inspection, while PSI often refers to an inspection performed when the order is substantially completed and packed. The buyer should define the timing, sampling method, checklist, and release criteria.
No.
AQL is a parameter used within an acceptance-sampling plan. It helps determine sample size and acceptance/rejection numbers for a lot; it is not a guarantee of the actual defect rate in the shipment.
No.
An approved sample is useful as a physical reference for appearance, configuration, and basic user-perceived characteristics. It cannot define component versions, tolerances, inspection methods, sampling rules, or compliance requirements by itself.
No.
PSI provides sampled evidence of conformity at a particular time. It does not prove cycle life, drop resistance, battery endurance, long-term waterproof performance, or other reliability characteristics that require separate validation.